 Türkçe
 English
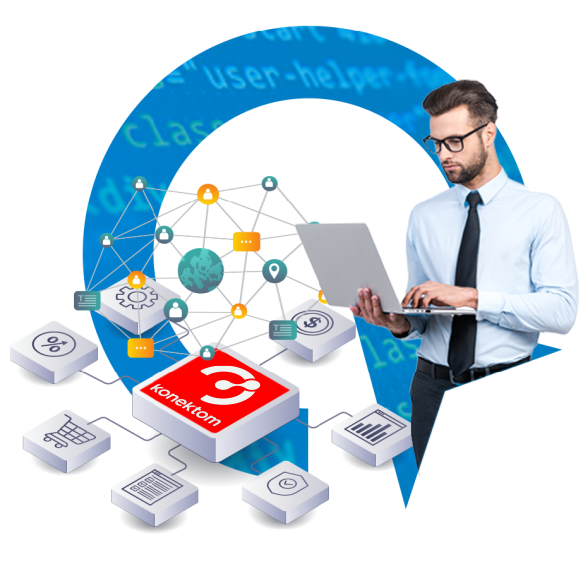
The chemical industry demands the most precise management of production processes due to both complex process structures and high safety and quality standards. Throughout the process, from raw materials to the final product, numerous critical parameters such as temperature, pressure, time, and chemical ratios must be monitored and managed in real-time. The Manufacturing Execution System (MES) , which enables the digital control of this complex system, acts as a digital nervous system for the chemical industry.
MES solutions collect real-time data from the field, making the entire production process end-to-end monitorable and optimizeable, from production planning and quality management to equipment efficiency and energy consumption.
1. Digitalization in Production Processes with MES
Production Planning: Time and Resource Management in Chemical Processes
The production planning module, which sequences production orders in the most efficient way according to raw materials, equipment, and manpower, reduces transition times, optimizes process times, and minimizes production errors.
Equipment Integration: All Processes from Reactors to Filling Lines are in Harmony
Thanks to its integration with automation systems such as SCADA, PLC, and DCS, all equipment is monitored from a central location, ensuring an automated production process.
Data Collection and Processing: Digital Security of Process Data
All process data, such as temperature, pH, and pressure, are collected and analyzed in real-time to evaluate quality, efficiency, and safety.
Business and Production Monitoring: Real-Time Observation, Immediate Response
All operations along the production line can be monitored in real-time, allowing for the detection of delays or deviations and enabling quick intervention.
Organizational Efficiency (OEE): The Path to Excellence in Chemical Plants
OEE calculations are performed by analyzing machine downtime, performance losses, and quality ratios; this ensures the most efficient use of equipment.
Reporting & Analysis Management: A Data-Driven Approach for Decision Support
Production, quality, and energy data are visually presented in dashboards. This provides strategic analysis and decision support for senior management.
Alarm and Alert Management: Detect Immediate Threats Proactively
This system, which automatically generates alarms when critical values are exceeded, warns operators, preventing workplace accidents and production errors.
Quality Management: Consistent Production in Accordance with Standards
It digitizes the quality control processes for chemical products; analysis results, specifications, and conformity data are automatically tracked.
Energy Management Module: Efficient and Sustainable Chemical Production
By monitoring energy data such as electricity, natural gas, and steam consumption, energy efficiency is increased, and contributions are made to sustainability goals.
2. Benefits of Using MES in the Chemical Industry
- Real-time data monitoring enhances process control.
- Traceability makes product recalls easier.
- Product quality is standardized through recipe management .
- Human error is minimized, and production safety is increased.
- Equipment and labor efficiency are maximized.
In conclusion, Centra MES solutions in the chemical industry digitize production processes while maximizing quality, efficiency, and safety. In this highly competitive sector, businesses that embrace digitalization become both more agile and achieve sustainable success.